AnyPCBA PCB and PCBA case studies

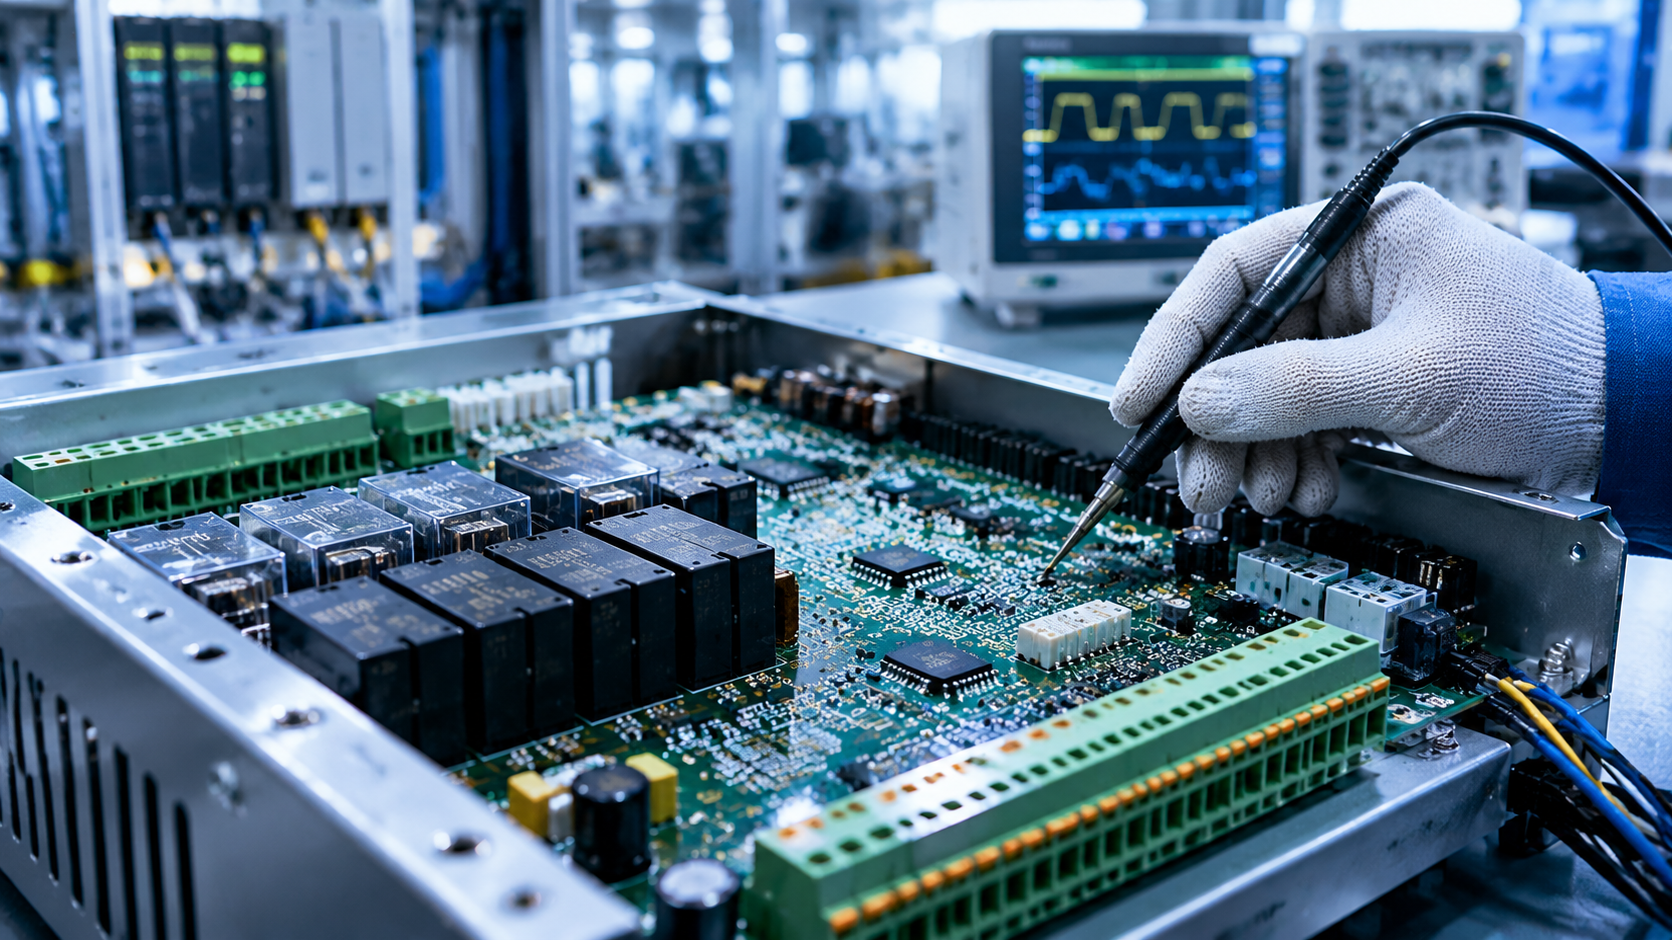
Introduction: A real-world case study of an industrial PLC that suffered from signal glitches and communication dropouts due to electromagnetic interference. The solution: an 8-layer PCBA redesign with a symmetric stack-up, dedicated ground planes, strategic component placement, and thermal via arrays—achieving stable operation in a harsh industrial environment.
Description: Based on AnyPCBA's small-to-medium volume PCBA manufacturing experience, this case study explains how an 8-layer PCBA design solved EMI and thermal challenges in an industrial PLC—covering stack-up structure, component placement, and manufacturing process control.
In late 2025, a customer specializing in automation equipment approached us.
Their previously stable PLC (Programmable Logic Controller) began experiencing sudden, erratic failures when multiple production line machines started simultaneously—input signals jumped, Ethernet communication dropped, and the program even crashed.
After two weeks of troubleshooting, no software bugs or loose wiring were found. The root cause was finally identified: the traditional 2-layer PCBA could no longer withstand the "electromagnetic storm" generated by on-site inverters and relays.
To solve this fundamentally, the customer decided to abandon the 2-layer board and switch to an 8-layer ENIG PCBA, achieving a system-level redesign of "small size + high reliability" within the extremely limited space of a distribution cabinet.
In a compact PLC, several conflicting modules are often integrated:
High-frequency digital system: MCU, RAM, Flash operating above 200MHz.
High-noise power circuit: relay/transistor outputs generating massive di/dt spikes during switching.
Sensitive analog channels: AD/DA sampling, where even a few mV of coupled noise on the reference voltage causes distortion.
If all of this is crammed onto a 2-layer board, the result is: analog readings jumping like an ECG, CAN communication dropping frames every few minutes, and the watchdog constantly resetting.
Multilayer boards are not about "routing more traces"—they are about smarter functional isolation and reference plane construction. The final 8-layer stack-up was:
| Layer | Name | Function |
|---|---|---|
| L1 | Top Signal | MCU, memory, buttons, LEDs, some digital I/O |
| L2 | GND1 | Primary ground plane, solid copper, no splits |
| L3 | Signal High-Speed | Ethernet RMII, SPI Flash, JTAG signals |
| L4 | Power (+24V / +3.3V) | Dual power plane, partitioned supply |
| L5 | GND2 | Auxiliary ground plane, dedicated to analog and PHY |
| L6 | Analog & Mixed | ADC front-end conditioning, voltage reference, RS-485 transceiver |
| L7 | Signal Low-Speed | DO drive signals, optocoupler isolation links |
| L8 | Bottom Thermal | Relay bottom thermal pad, connected to GND |
Key design points:
Two complete ground planes (L2, L5) sandwich the signal layers, forming a stripline transmission mode that significantly suppresses crosstalk.
The L4 power plane is partitioned (+24V for IO supply, +3.3V for core logic), connected at a single point to prevent noise coupling.
L8 serves as the thermal layer, connected through 20 × Ø0.3mm microvias to L2/L5 ground planes, reducing relay bottom temperature rise by 18°C compared to a similar 2-layer board.
MCU placed in the center: shortens trace length to all peripherals.
ADC front-end kept away from relay drive area: at least 10mm isolation.
PHY chip placed close to the RJ45 connector: reduces external interference.
DC-DC module placed at the edge: improves heat dissipation and reduces internal circuit impact.
All high-speed signal traces routed on L3/L6 inner layers, avoiding surface exposure that turns traces into antennas.
No additional shielding enclosure needed: the multilayer structure itself provides excellent EMI suppression, saving approximately ¥80 per unit.
Efficient thermal management: the large thermal pad under the relay, combined with the microvia array, keeps temperature rise 18°C lower than a comparable 2-layer board.
Remote maintenance support: built-in watchdog and self-diagnostics allow runtime status reporting via Modbus, reducing fault location time by 70%.
Long-term reliability: OSP + ENIG hybrid surface finish balances solderability and contact durability. The complete unit passed HALT testing.
During DFM review at AnyPCBA, we frequently see engineers use multilayer boards but still encounter failures. Here are hard-learned rules from real projects:
During PCB lamination, resin flow and stress distribution must be balanced. An asymmetric stack-up causes board warpage, especially during reflow, which can lead to BGA cold joints.
AnyPCBA recommendation: Use a symmetrical structure, ensuring dielectric thickness and copper weight are balanced top and bottom.
A standard through-via has about 1–2nH of parasitic inductance. For high-speed signals (above 100MHz), this is enough to cause reflection and ringing.
AnyPCBA recommendation: Use blind/buried vias (HDI process) for high-frequency signals. Use via-in-pad for power decoupling capacitors to minimize lead length.
Many beginners hear "separate analog and digital ground" and immediately cut through the GND layer. The result is a larger ground loop and more noise.
AnyPCBA recommendation: If separation is necessary, connect at a single point (star point grounding), usually near the ADC or power entry. It's often best to start with a unified ground plane and rely on proper layout to avoid interference.
Characteristic impedance depends on trace width (w), spacing (s), dielectric thickness (h), and dielectric constant (εr).
AnyPCBA recommendation: Use professional tools like SI9000 or Saturn PCB Toolkit. During DFM review, the factory will confirm stack-up parameters with you to ensure production hits your impedance target.
Power devices (DC-DC, MOSFETs) must have a thermal pad underneath, connected through multiple vias to inner ground copper.
AnyPCBA recommendation: Determine via count based on thermal simulation results, and be aware that excessive copper area can cause cold joints during soldering due to rapid heat dissipation.
This case is one of AnyPCBA's typical experiences in industrial control and high-reliability PCBA manufacturing.
In this project, AnyPCBA was involved in:
8-layer stack-up structure review: confirming L4 power plane partitioning and lamination process windows
Microvia array process confirmation: drilling precision and hole wall quality for Ø0.3mm thermal microvias under relays
Hybrid surface finish process: compatibility control of OSP and ENIG on the same board
HALT reliability testing support: working with the customer to complete thermal cycling and vibration shock testing
Our manufacturing capabilities cover 2–64 layers, including HDI, rigid-flex, and high-frequency hybrid. We hold ISO 13485 (medical) and IATF 16949 (automotive) certifications, with extensive experience in industrial PLCs, servo drives, inverters, and other high-interference environments.
If you're working on industrial control PCBA design, or facing similar EMC and thermal bottlenecks, contact us through our website. Our engineers can help you anticipate stack-up and manufacturing risks during DFM review.


